


The manufacturing process of titanium tees
View More
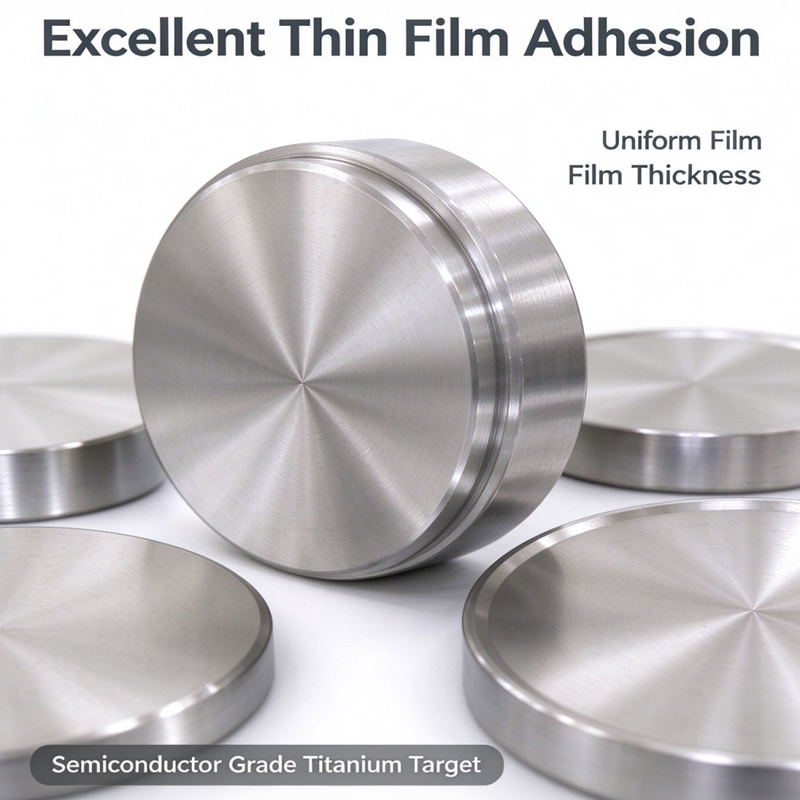
If you're constantly battling film thickness variation, uneven target erosion, or particle defects, don't rush to adjust your process parameters. In many cases, the root cause isn't the tool or the gas lines—it's the grain size and microstructure of the titanium target itself.
This article focuses on that one point. We won't go into purity, bonding, or gas impurities—just grains.
Why Does Grain Size Matter So Much?
A titanium target is a polycrystalline material. Think of it as a road paved with countless small stones—each stone faces a different direction, and each has a different sputtering yield. The coarser and more randomly oriented the stones, the greater the local variation in sputtering rate.
When grain size exceeds a certain threshold (typically >100 μm), selective sputtering becomes obvious on the target surface: some grains sputter quickly and get hollowed into pits; others sputter slowly and build up as ridges. Once the surface topography becomes uneven, the plasma is disturbed as well, and film thickness deviation is amplified.
In semiconductor barrier layers (Ti/TiN) and high-generation display coatings, this thickness deviation directly translates into sheet resistance uniformity and step coverage. At nodes below 5 nm, process parameter adjustments alone can barely compensate.
So grain control is not a "nice-to-have"—it is a prerequisite for film uniformity.
Four Metrics to Watch When Sourcing
① Average grain size
Semiconductor-grade titanium targets typically require ≤50 μm, and high-demand applications can achieve 20–30 μm. Decorative coating targets can be relaxed to within 100 μm.
② Grain size distribution
Don't look only at the average. Standard deviation matters just as much. Even a small number of abnormally coarse grains can cause local sputtering behavior to shift abruptly. Acceptance should consider both maximum grain size and distribution uniformity.
③ Grain orientation (texture)
Titanium has a hexagonal close-packed structure, and sputtering yields differ significantly between crystal planes. Too scattered a texture leads to high sputtering rate variability; an overly concentrated texture can cause uneven target erosion. What engineering wants is a controllable and uniform texture distribution—not the most concentrated one possible.
④ Density and porosity
If powder metallurgy routes are not fully sintered, residual porosity becomes "hot spots" during sputtering, causing local overheating and particle shedding. Density is generally required to be ≥99.5%.
Three Process Routes—How to Choose?
Cast metallurgy (VAR/EBM → thermomechanical processing)
Grain size is typically 50–150 μm. Low cost, capable of large target sizes, mature batch consistency. But grains are coarse and uneven, making semiconductor-grade stability difficult. Suitable for decorative coatings, tool coatings, and general industrial coatings.
Powder metallurgy (CIP/HIP sintering)
Grain size can be controlled at 20–60 μm—fine and uniform, with low segregation and high density. The trade-off is a longer process chain and higher cost than casting, plus sintering uniformity challenges for large targets. Suitable for semiconductor barrier layers, optical coatings, and demanding display coatings.
Spark plasma sintering (SPS)
Grain size can reach <20 μm, with density >99.5%. Low-temperature rapid sintering provides good suppression of grain growth. However, equipment investment is high, part size is limited, and mass-production consistency is still being validated. Suitable for R&D and small-size, high-requirement targets.
How to Tell If a Grain Control Is Reliable
Look at metallography and EBSD. Metallography quickly reveals average grain size and abnormal grains; EBSD also provides grain size distribution and texture information—a practical acceptance tool for semiconductor-grade titanium targets.
Run small-scale sputtering validation. Meeting material specs does not mean meeting sputtering performance. Before bulk purchasing, measure target erosion profile and substrate film thickness distribution. Whether grain control is on point ultimately shows in the sputtering results.
Ask for traceable acceptance documentation. Average grain size and standard deviation, maximum grain size, density, texture distribution (if applicable), and sputtering validation data for the corresponding batch. Suppliers who can consistently provide these are usually more credible in process maturity.
Selection Advice
· If the end application is semiconductor or high-generation display: write grain size into the technical agreement as a core acceptance metric—don't specify purity alone.
· If the end application is decorative or tool coating: grain requirements can be relaxed, but keep an eye on abnormally coarse grains and density to avoid particle defects.
· When evaluating suppliers, traceable grain control data is more persuasive than a "high-purity" claim.
If you're dealing with film uniformity drift, uneven target erosion, or particle defects, send us your end application, target size, sputter equipment type, and current uniformity requirements, and we'll help you map out the corresponding grain metrics and acceptance checklist.
If you're ready to request a quote, a sample, or technical guidance on which titanium grade fits your project, reach out directly
Email: sales@globaltigroup.com
The team can walk through your specifications, confirm certifications, and arrange fast delivery for your next order.
Hello, I am the online customer service
